Loading Samarkand Store...
Official Online Store of Samarkand Laboratories, Pakistan
Nationwide Delivery · Cash on DeliveryCustomer Care
Our dedicated laboratory facility integrates clean-room pharmaceutical processing, botanical steam distillation, automated liquid bottling, and stringent analytical testing laboratories. Every formulation complies with national health standards and undergoes microbiological scrutiny.
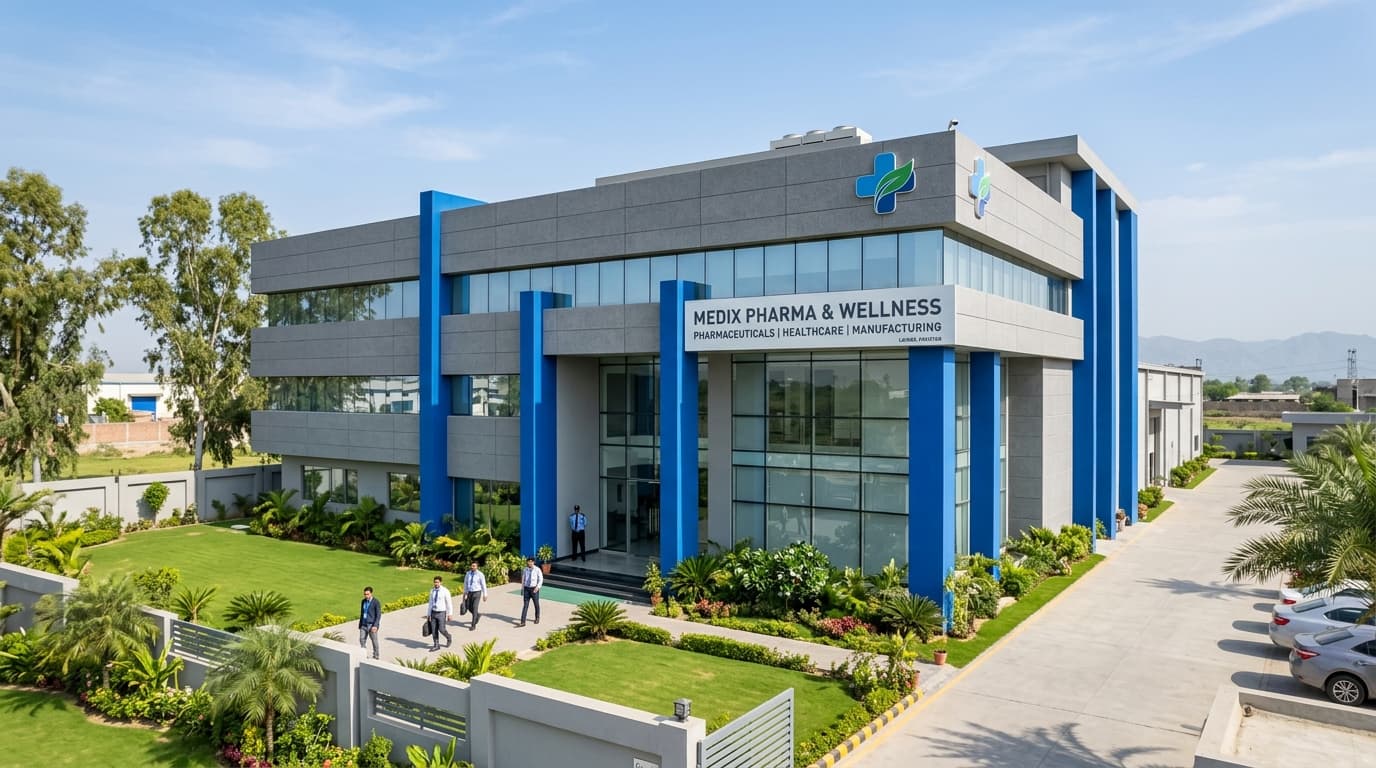
Modern clean-room operations and botanical processing facility in Pakistan.
Temperature-regulated mixing vats, homogeneous suspension blenders, and pharmaceutical-grade dosing units producing antacids and cough formulations.
Closed-loop steam distillation units extracting authentic floral water essences, notably our pure Arq-e-Gulab rose water, without thermal degradation.
Hygienic multi-head liquid fillers, induction foil cappers, and tamper-evident shrink sleeve applicators protecting product shelf stability.
Analytical chemistry stations evaluating specific gravity, pH balance, viscosity, and microbiological sterility before commercial lot release.
Shop select products manufactured in our laboratories with guest Cash on Delivery.